


Our production line, from raw material to finished product
We run the entire process in our own facility, from scrap to packed product. Click on a stage to see its details.
Scroll sideways to explore the diagram.
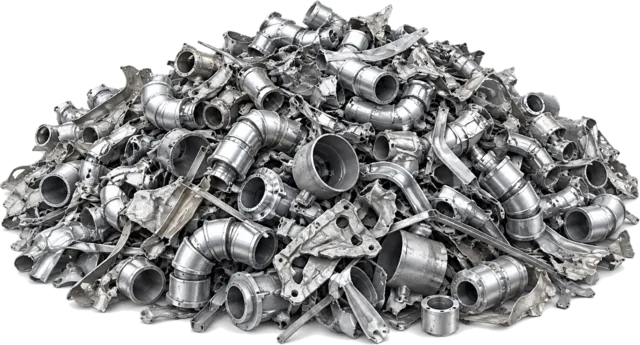
Aluminium Scrap
Aluminium scrap is remelted in the furnaces of our melt shop and returned to production. Aluminium keeps its properties when recycled, which makes scrap a key input for sustainable production.
- Melting furnaces
- 16 and 25 tonnes
- Recyclability
- 100%, infinitely

Aluminium Ingot
The main raw material of the casting line. High-quality ingots are melted in our melt shop, and the molten metal is refined and alloyed before casting.
- Melting furnaces
- 16 and 25 tonnes
- Alloy series
- AA 1XXX, AA 3XXX
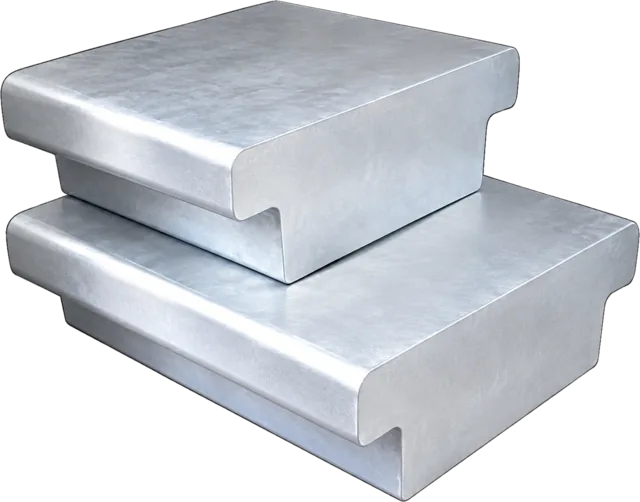
T-Bar
A large aluminium ingot with a T-shaped cross-section. It allows fast, high-tonnage charging of the melting furnaces.
- Form
- T-section ingot
- Melting furnaces
- 16 and 25 tonnes
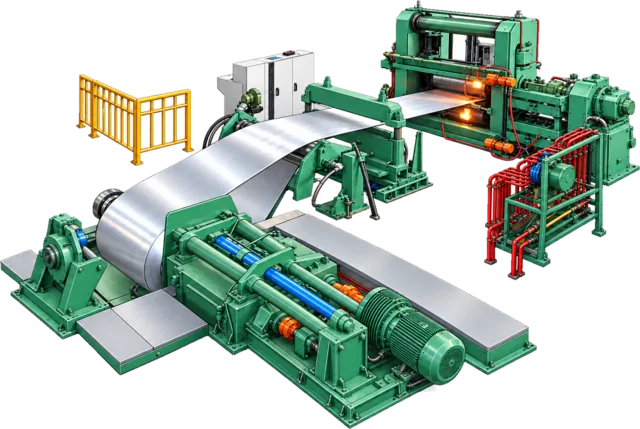
Melt Shop & Casting Line
Scrap, ingot and T-bar are melted in the furnaces of our melt shop, where the molten aluminium is refined and alloyed. On the continuous twin roll casting line it then passes between two rolls, solidifies into strip and is wound into coil.
- Melting furnaces
- 16 and 25 tonnes
- Technology
- Continuous twin roll casting
- Lines
- 2
- Thickness
- 4.00 – 8.00 mm
- Width
- 800 – 1650 mm
- Annual capacity
- 30,000 tonnes
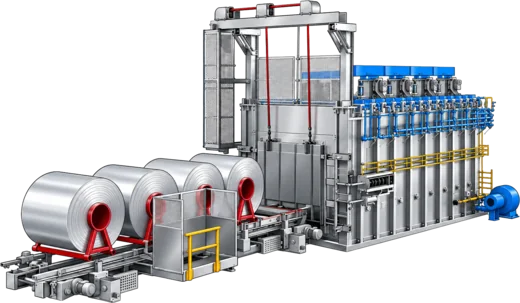
Annealing Furnace
Coils are annealed to reach the mechanical properties their application needs. Rolling and annealing are planned together, covering a wide temper range from soft to hard.
- Furnace capacity
- 50 tonnes
- Temper range
- H00 – H28
- Standard tempers
- H00, H12, H22, H14, H24, H16, H26, H18, H19, H28
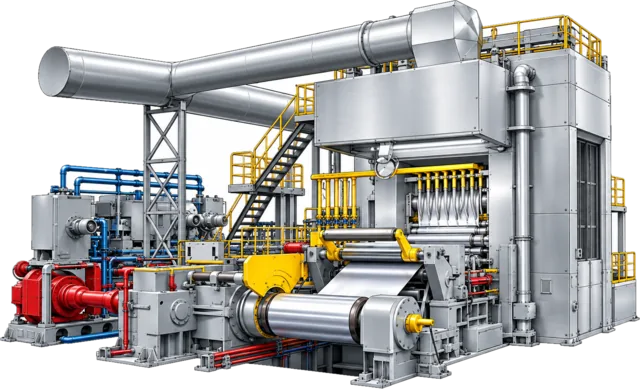
Cold Rolling Mill
Cast coil is passed between the rolls of the cold rolling mill, reduced step by step and rewound. The result is a tight thickness tolerance and a high-quality surface.
- Entry thickness
- 4.00 – 8.00 mm
- Exit thickness
- 0.20 – 3.00 mm
- Width
- 400 – 1250 mm
- Annual capacity
- 30,000 tonnes
Annealing Furnace
Coils are annealed to reach the mechanical properties their application needs. Rolling and annealing are planned together, covering a wide temper range from soft to hard.
- Furnace capacity
- 50 tonnes
- Temper range
- H00 – H28
- Standard tempers
- H00, H12, H22, H14, H24, H16, H26, H18, H19, H28
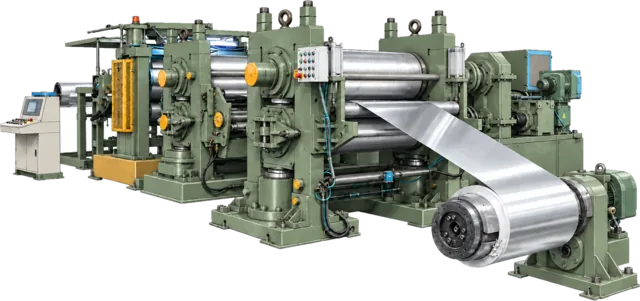
Washing, Tension Leveling & Embossing
Coils are cleaned on the washing–tension leveling–embossing line and passed through polymer tension rolls to obtain an ideal strip profile. On request, classic stucco or diamond patterns are embossed on the same line.
- Surface
- Plain, stucco, diamond
- Embossed thickness
- 0.20 – 1.00 mm
- Width
- 400 – 1250 mm
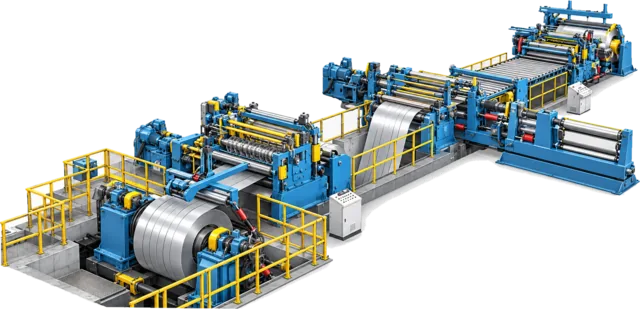
Slitting
Coils are slit into strips of the required widths on precision slitting lines and rewound. Burr-free edges and tension-free winding make the strip ready for automatic feeding lines.
- Width
- 35 – 400 mm
- Thickness
- 0.20 – 2.50 mm
- Inner diameter
- 508 mm (20")
- Outer diameter
- max. 1700 mm
- Surface
- Plain (embossed on request)
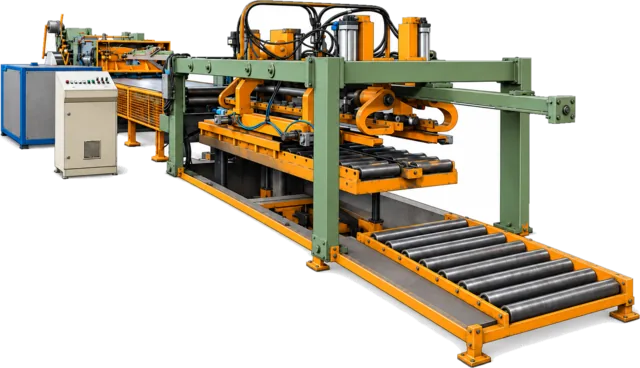
Cut-to-Length
Coil is cut to the ordered length on the cut-to-length line, turned into sheet and stacked. Besides standard stock sizes, custom project sizes are produced.
- Width
- 250 – 1250 mm
- Length
- 350 – 4200 mm
- Thickness (plain)
- 0.20 – 3.00 mm
- Thickness (embossed)
- 0.30 – 1.00 mm
Packing & Shipment
Coils are shipped on wooden pallets, wrapped in stretch film and kraft paper and secured with steel straps; coil orientation is eye-to-wall or eye-to-sky. Sheets are stacked flat on wooden pallets with protective paper between them; packs are stretch-wrapped and steel-strapped, and the top surface is protected with a wooden cover. A protective PE film can be applied to the sheet surface on request. Narrow strips are stacked with separators to prevent edge contact.
- Packing
- Wooden pallet, stretch and kraft wrap, steel straps
- Coil orientation
- Eye-to-wall or eye-to-sky
- Sheet
- Wooden pallet, flat stack with interleaving paper, stretch wrap and steel straps, wooden cover; PE film on request